很多厂长抱怨:几万块的主机开着,工人身边还是一层白雾。问题很少出在滤筒本身,而是吸尘罩、管道、风量这三件事在进场前没对齐。
Many factory managers complain that with the tens of thousands of yuan mainframe on, there is still a layer of white mist around the workers. The problem rarely lies in the filter cartridge itself, but rather in the misalignment of the vacuum hood, pipes, and air volume before entering the site.
先分场景再定结构。单台打磨机、切割位,用单机脉冲就行,省管道;整条流水线、十几个工位同时起尘,才值得上中央系统。别为了“看起来整齐”把三个相距20米的工位硬拉一根长管,阻力上来后末端基本没吸力。
Divide the scene first and then determine the structure. A single polishing machine and cutting position can be used with a single pulse, saving pipeline costs; Only when the entire assembly line and more than ten workstations are dusty at the same time, is it worth going to the central system. Don't forcefully pull a long pipe from three workstations that are 20 meters apart just to "look neat", as there is almost no suction at the end when the resistance comes up.
风量不是查表抄的。每个罩口要先算控制风速(通常1~3m/s),再乘罩口面积;多工位按“同时使用系数”叠加,别把所有点位风量简单相加。开放车间、无围挡工位,总风量再留15%~25%余量,不然粉尘一扩散就抓不住。
The air volume is not recorded by checking the table. Each hood opening needs to first calculate the controlled wind speed (usually 1-3m/s), and then multiply it by the hood opening area; Overlay multiple workstations according to the "simultaneous use factor", do not simply add up the air volume at all points. Open the workshop and open the workstations without enclosures, leaving a margin of 15% to 25% for the total air volume, otherwise the dust will not be captured once it spreads.
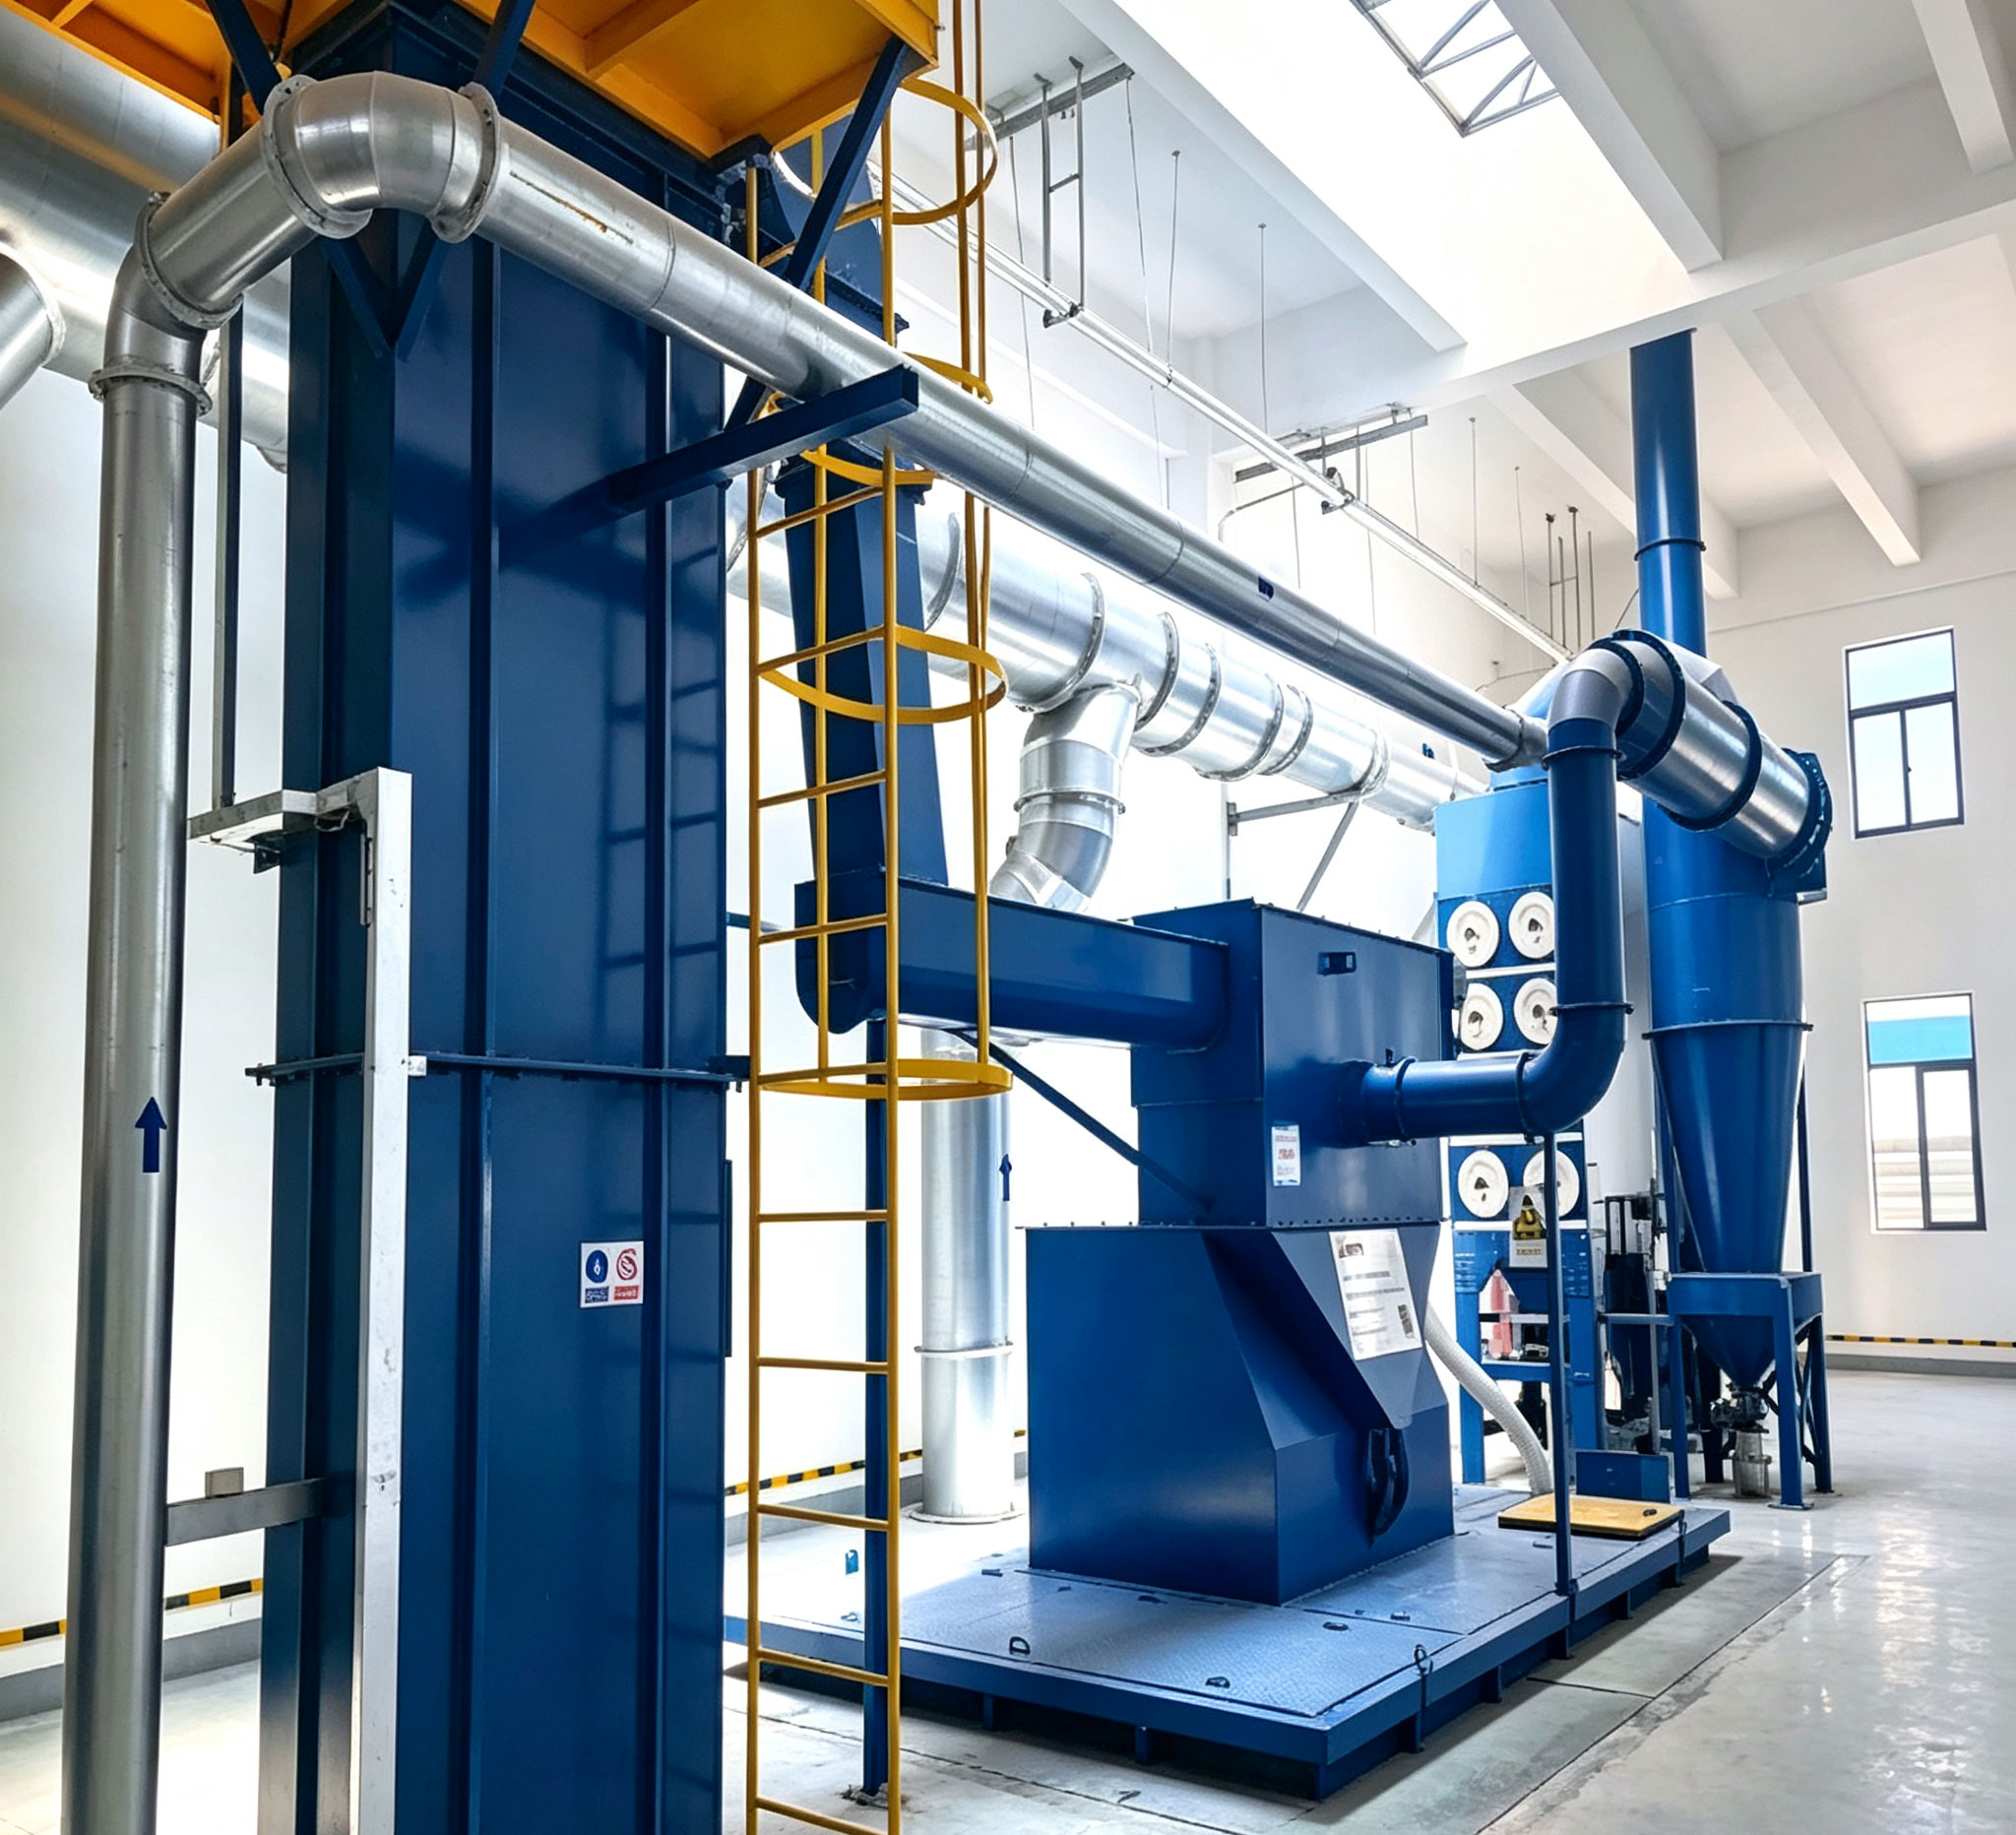
管道比主机更吃功力。主管风速控制在15~22m/s,太低沉降堵管,太高磨损尖叫;支管接主管用30°~45°斜三通,别垂直开孔。弯头用大半径,一个直角弯头差不多吃掉3~5米直管阻力。长管道必须做渐缩管,不然远端工位永远吸不动。
Pipelines require more power than hosts. The wind speed of the supervisor should be controlled at 15-22m/s. If the settlement is too low, the pipe will be blocked, and if it is too high, it will wear out and scream; Use a 30 °~45 ° diagonal tee for connecting the branch pipe to the main pipe, and do not drill vertically. Bend with a large radius, a right angle bend can consume approximately 3-5 meters of straight pipe resistance. Long pipelines must be made with tapered pipes, otherwise the remote workstation will never be able to suction.
过滤风速别被销售带偏。同样标10000风量,滤筒面积小、风速拉到1.5m/min以上,糊筒和脉冲阀罢工是早晚的事。细粉尘走滤筒时风速压到0.6~1.0m/min,布袋也不过1.2m/min左右,面积给够才省电省滤芯。
Don't get the filtering wind speed biased by sales. With the same air volume of 10000, a small filter cartridge area and a wind speed of over 1.5m/min, it is only a matter of time before the paste cylinder and pulse valve strike. When the fine dust passes through the filter cartridge, the wind speed should be maintained at 0.6~1.0m/min, and the cloth bag should only be around 1.2m/min to save energy and filter cartridges.
防爆和结露是隐藏项。铝镁、木工粉尘必须配火花探测、隔爆阀和防静电滤材;温差大的厂房灰斗加伴热、箱体做保温,否则凌晨停机一小时,早上滤筒板结给你看。
Explosion proof and condensation are hidden items. Aluminum magnesium and woodworking dust must be equipped with spark detection, explosion-proof valves, and anti-static filter materials; Add heat tracing to the ash hopper and insulation to the casing of the factory building with large temperature differences, otherwise the machine will be shut down for one hour in the early morning, and the filter cartridge plate will be shown to you in the morning.
运维只盯一个数:进出风口压差。超过1200~1500Pa还硬跑,不是电机过载就是排放超标。每周看一眼脉冲阀喷气声、每月清一次灰斗,比一年大修一次划算得多。
Operations only focus on one number: the pressure difference between the inlet and outlet. Running hard beyond 1200~1500Pa is either due to motor overload or excessive emissions. Checking the pulse valve jet sound once a week and cleaning the ash hopper once a month is much more cost-effective than having a major overhaul once a year.
把“罩口抓得住、管道送得到、滤速压得低、压差盯得牢”这四句钉在开机表上,车间能见度会自己说话。
Nail the four sentences of "hold the mask tightly, deliver the pipeline, lower the filtration rate, and keep a close eye on the pressure difference" on the startup table, and the visibility in the workshop will speak for itself.
 : 18563723072
 : sdcjtz@126.com
 : 山东省德州市齐河县经济开发区名嘉西路9号
扫码添加微信了解更多

 公司简介
 荣誉资质
 合作伙伴
 发展历程
 公司优势
 企业环境
 服务办事处
 创杰动态
 行业动态
 鲁公网安备 37142502000144号