上自动喷涂线,老板常以为“买台六轴机器人”就自动出良品。真调试起来,橘皮、流挂、内腔漏底,比人工还费漆。问题不在机器人轴数,在整条工艺链没对齐。
On the automatic spraying line, the boss often thinks that "buying a six axis robot" will automatically produce good products. When it comes to debugging, orange peel, sagging, and internal cavity leakage are even more expensive than manual labor. The problem lies not in the number of robot axes, but in the misalignment of the entire process chain.

先选主机形态,不盲目堆配置:
Choose the host form first, do not blindly configure the heap:
平板、家电壳、规则件:伺服往复机,节拍稳、投入低;
Tablet, home appliance casing, regular components: servo reciprocating machine, stable cycle time, low input;
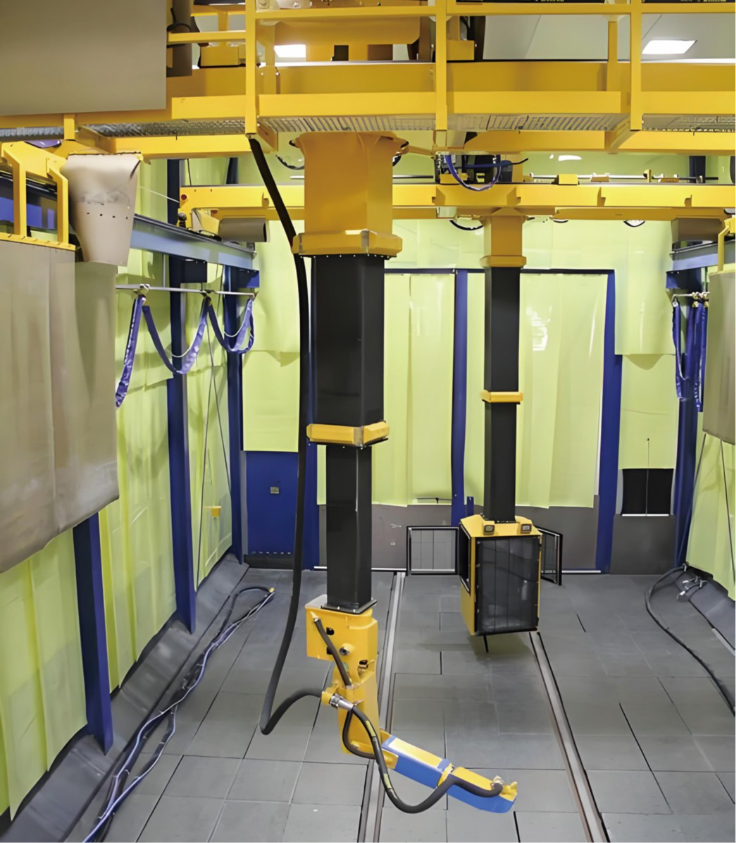
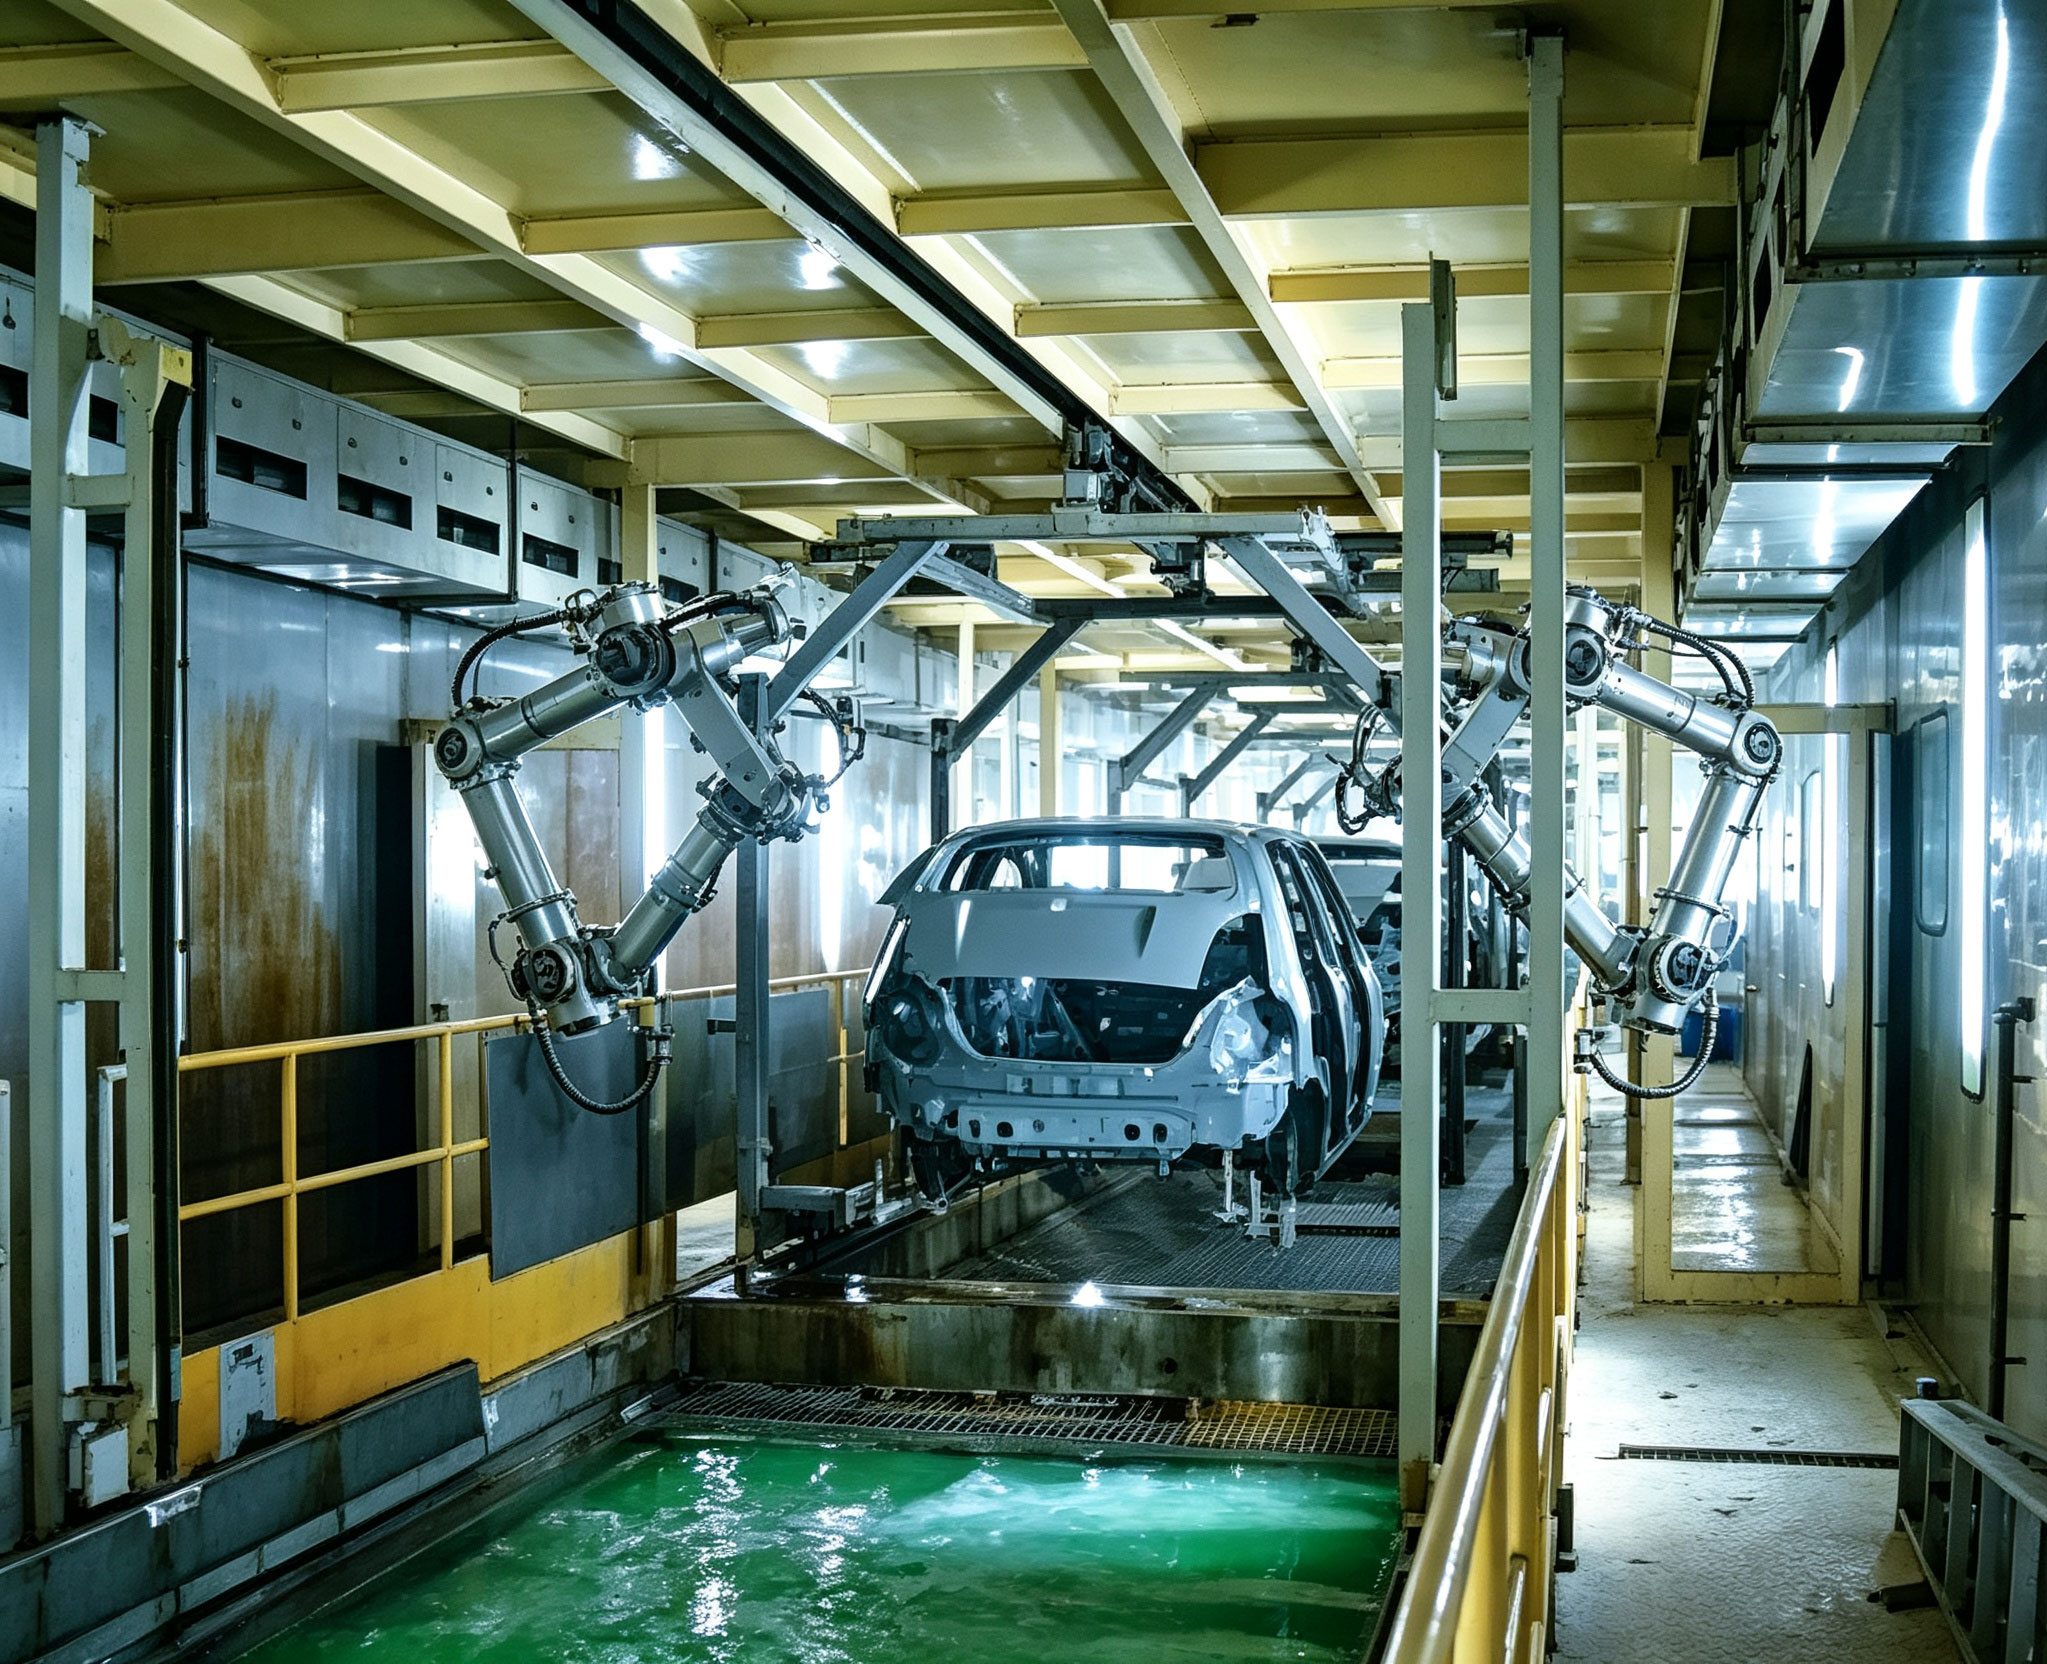
异形曲面、内凹、多款式小批量:六轴喷涂机器人,配转台/变位机消死角;
Irregular surface, concave, multi style small batch: Six axis spraying robot, equipped with turntable/positioner to eliminate dead corners;
负载别贪大,工件+治具占额定负载30%–60%区间,轨迹更稳、能耗更合理。
Don't be too heavy with the load. The workpiece and fixture account for 30% -60% of the rated load range, resulting in a more stable trajectory and reasonable energy consumption.
雾化方式先于机器人定型:
The atomization method takes shape before the robot:
多色小批、外观件:空气喷枪/HVLP,换色灵活;
Multi color small batch, appearance parts: air spray gun/HVLP, flexible color change;
大件导电件、省漆优先:静电旋杯,涂料利用率明显高,但要解决法拉第笼内腔偏薄问题;
Priority should be given to large conductive parts and paint saving: electrostatic spinning cup, significantly high paint utilization rate, but the problem of thin inner cavity of Faraday cage needs to be solved;
水性漆走静电,要做等电位与隔离处理,别直接套溶剂型参数。
Water based paint generates static electricity and requires equipotential and isolation treatment. Do not directly apply solvent based parameters.
整线八环节任一处掉链子都返工:
Any chain drop in any of the eight links of the entire line will be reworked:
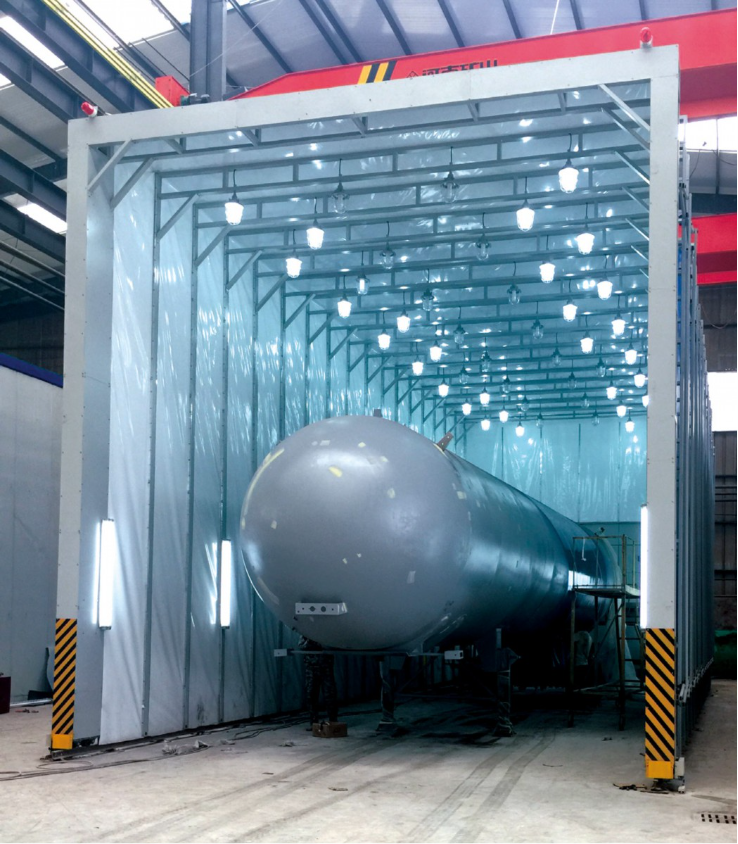
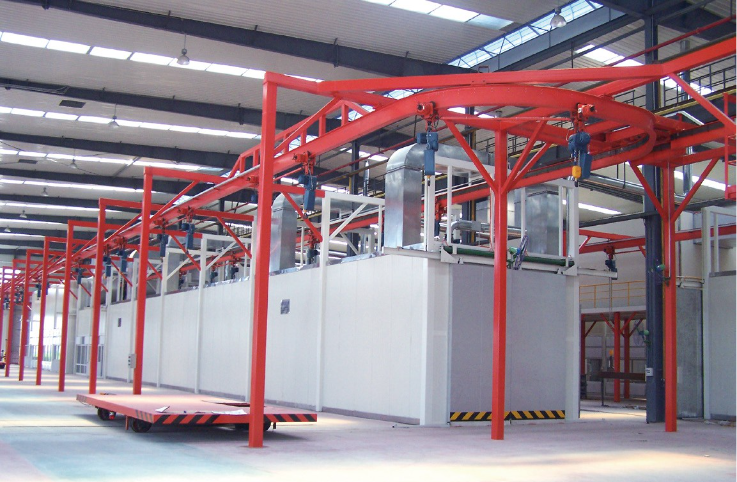
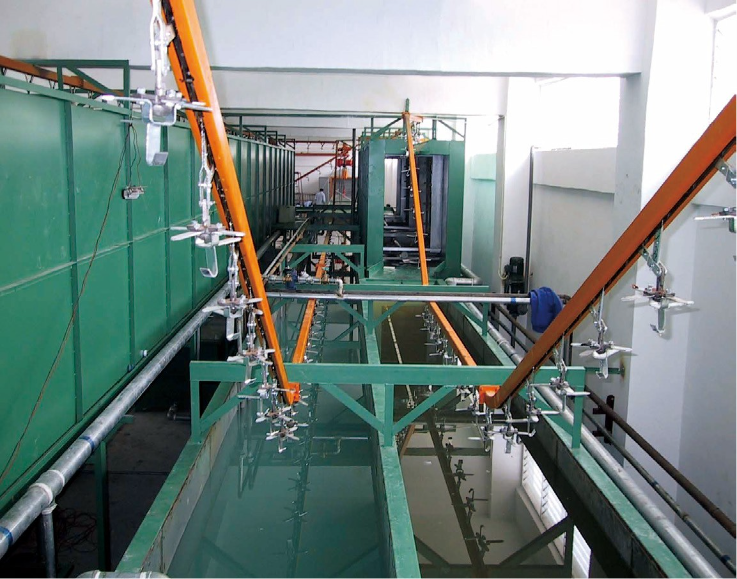
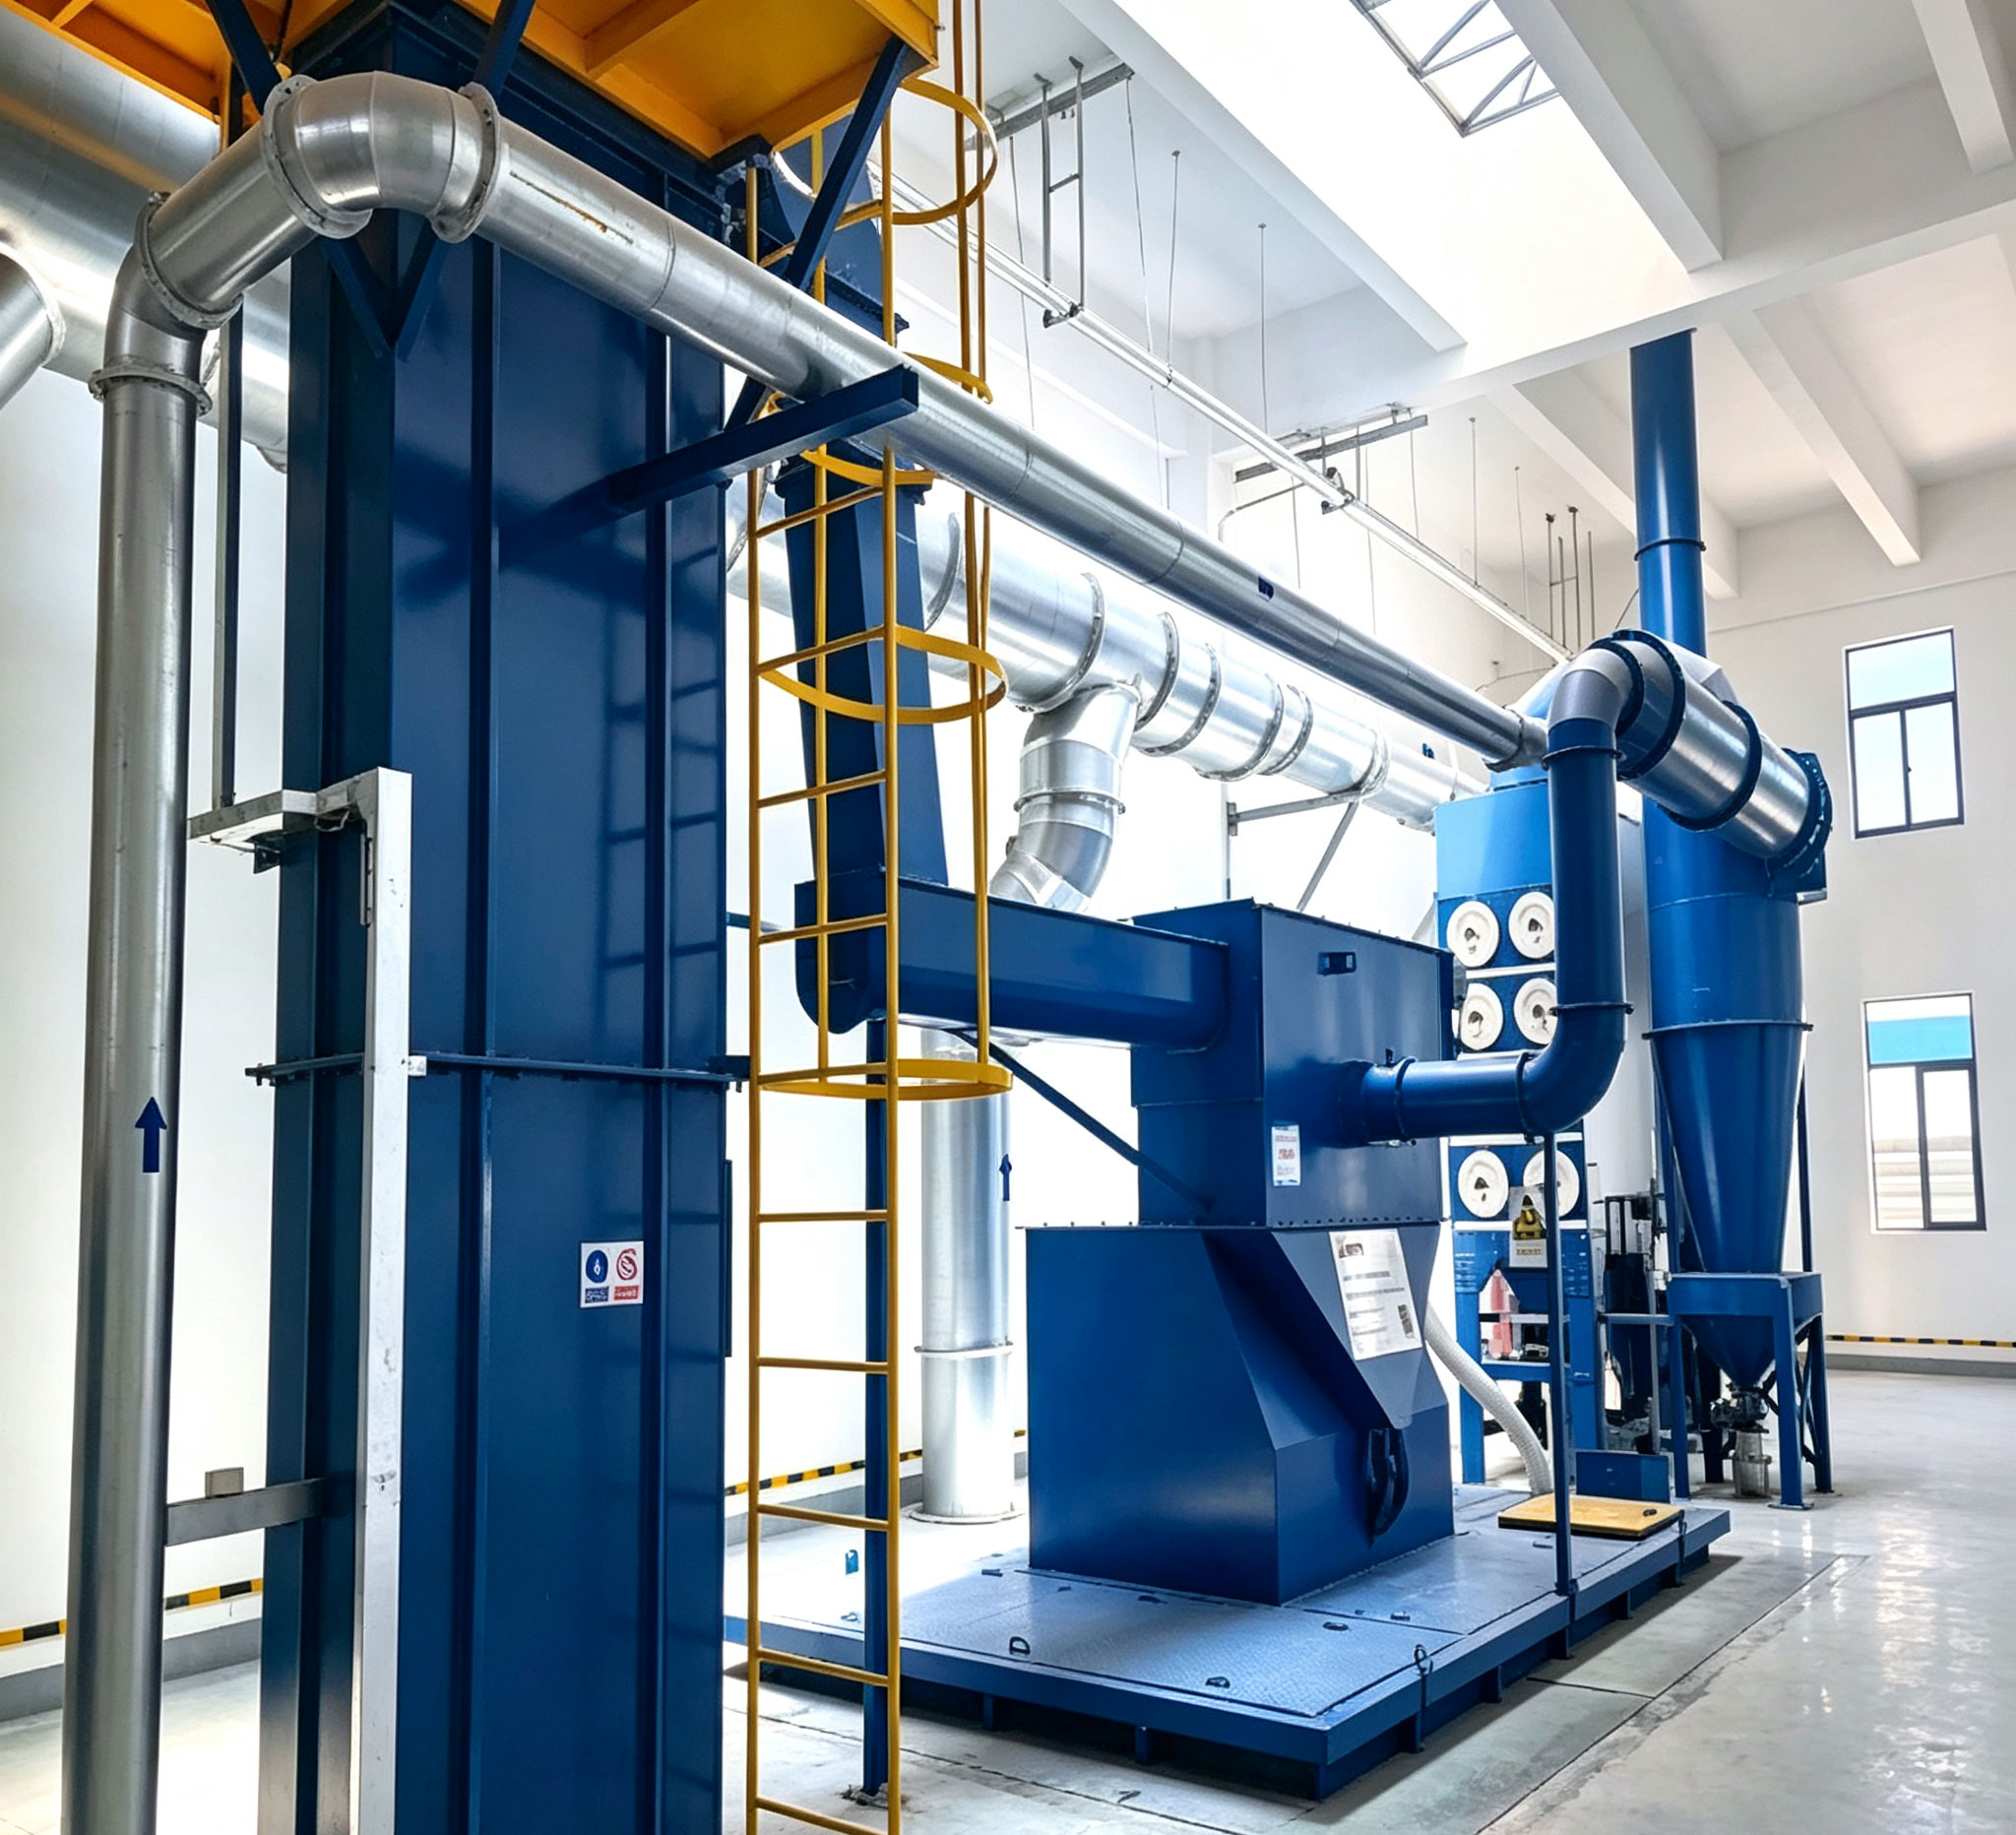
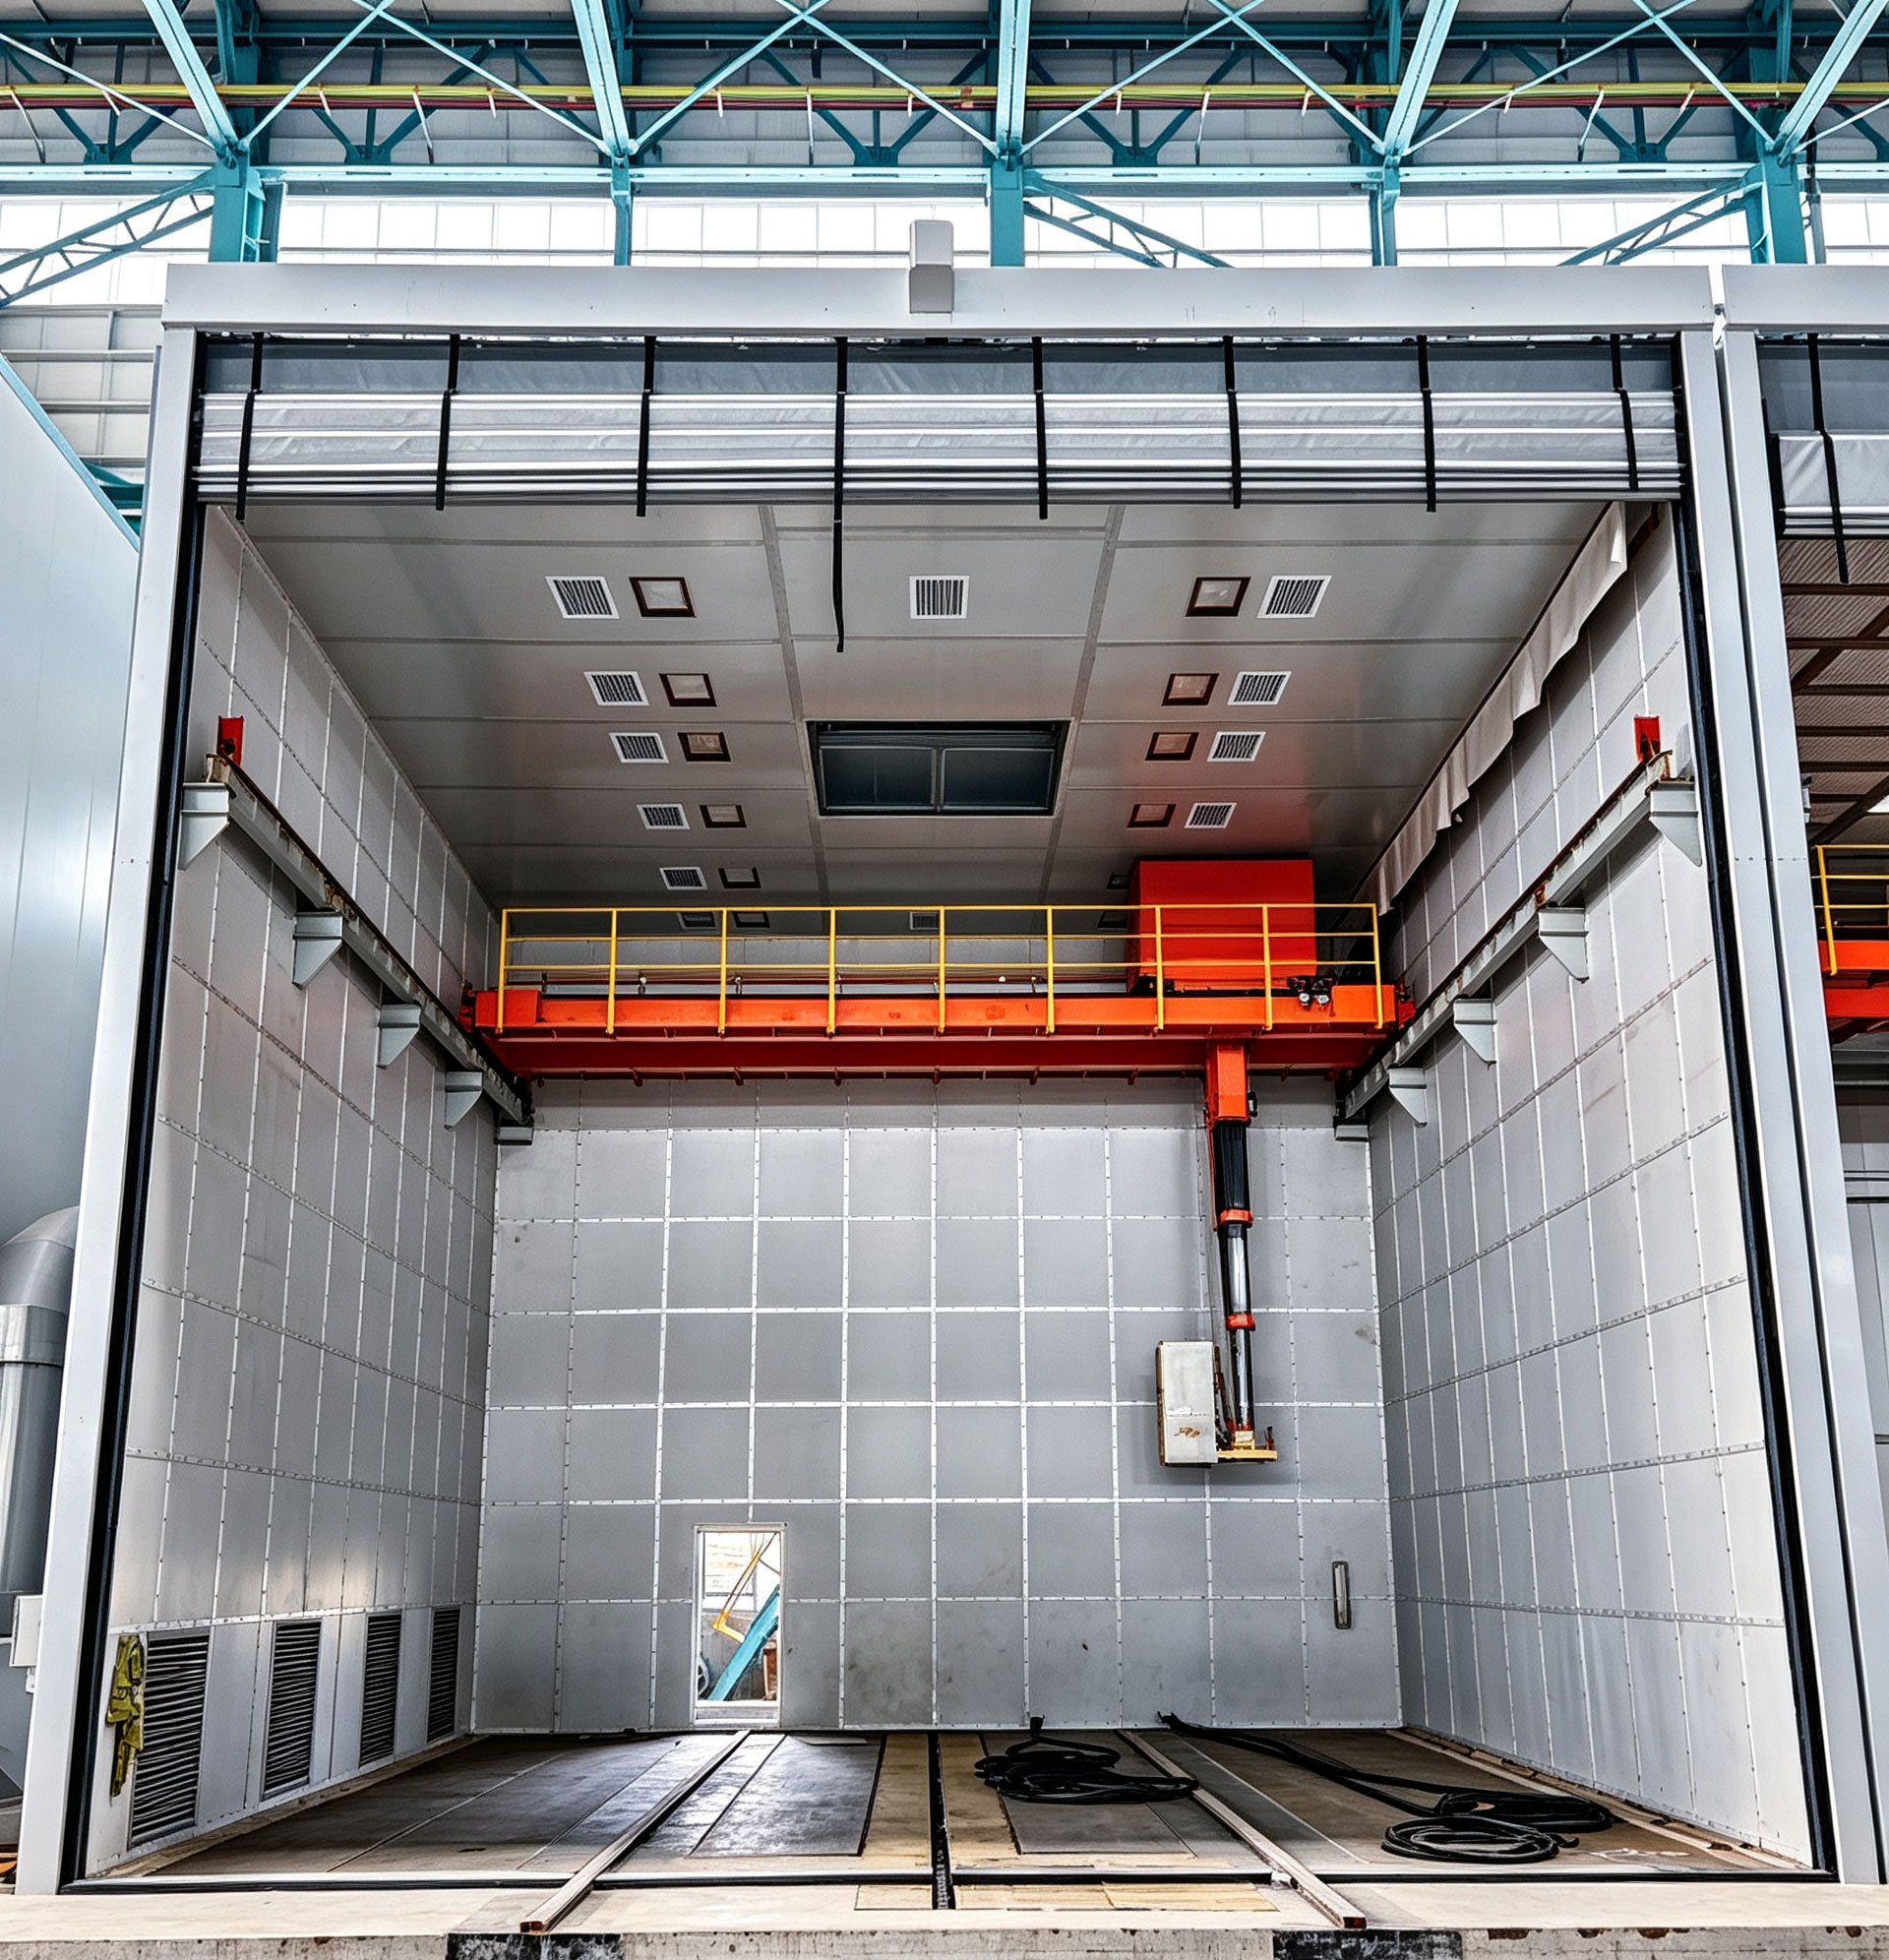
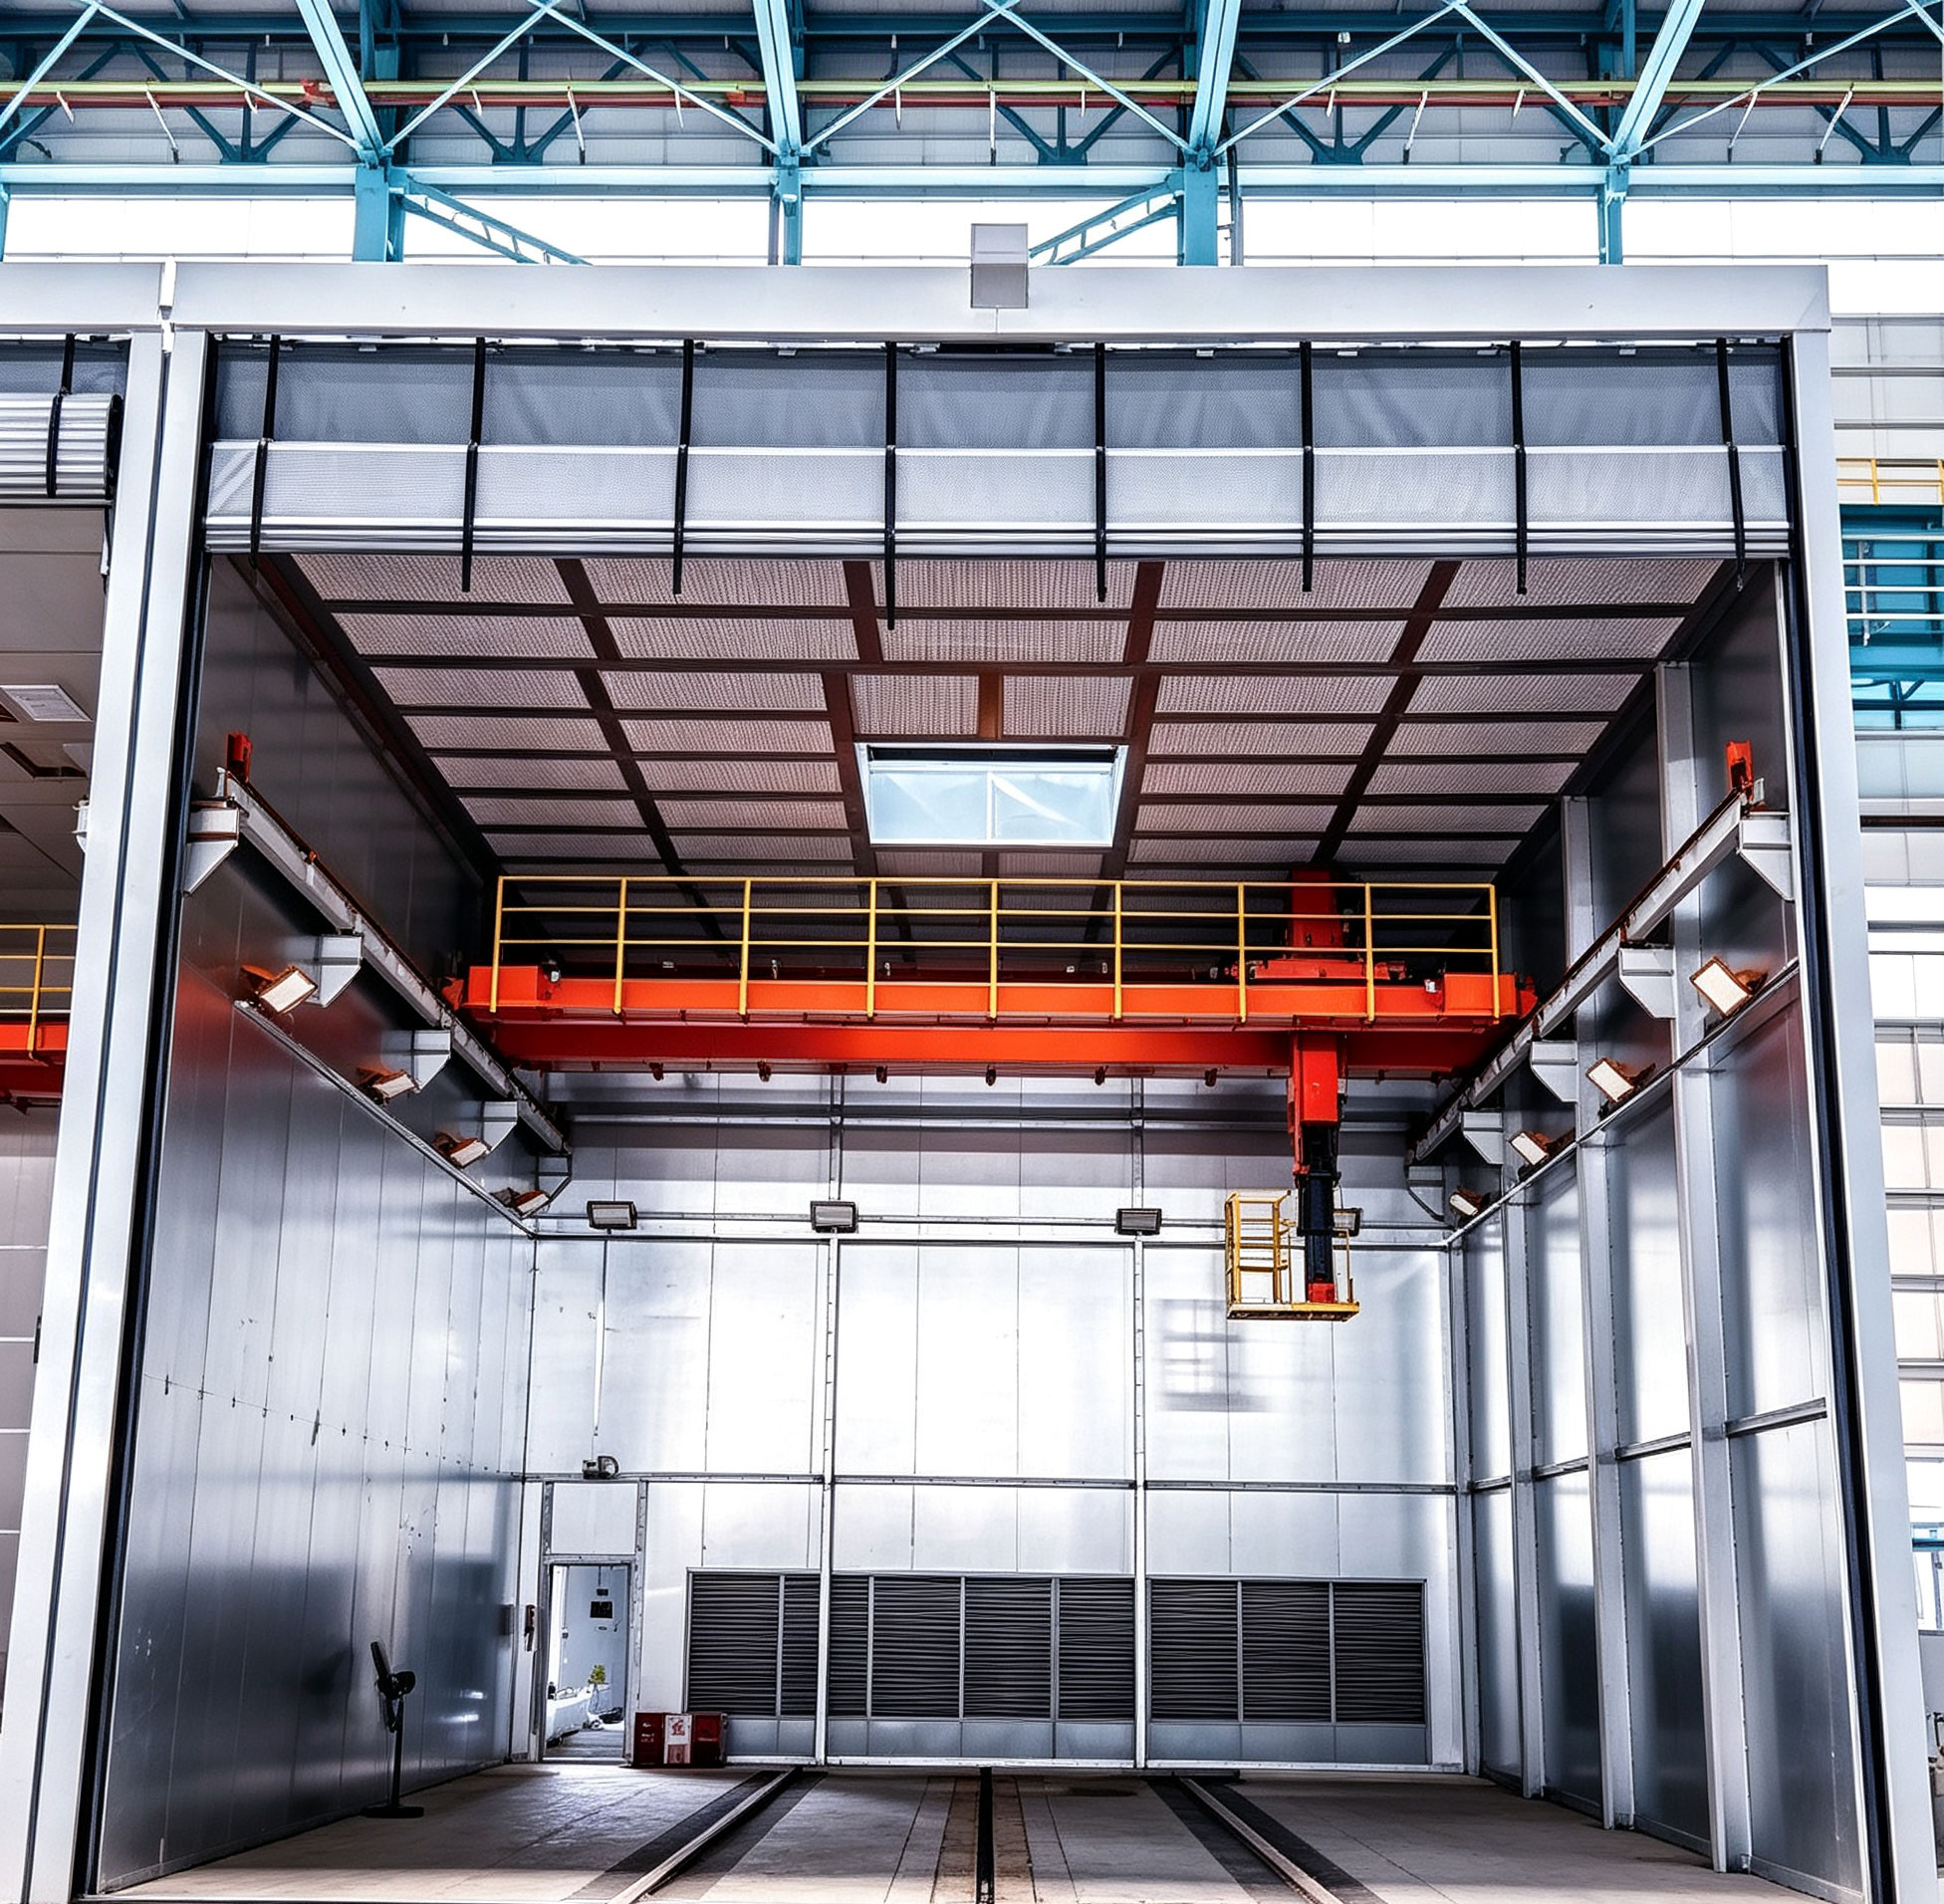
前处理除油除尘→喷房微负压与断面风速稳定→供漆压力/黏度闭环→机器人枪距搭接恒定(喷幅搭接约50%–75%)→流平→固化炉温曲线→VOCs处理→PLC总控联动。通风没启动不能喷,门联锁不能短接,这是合规底线。
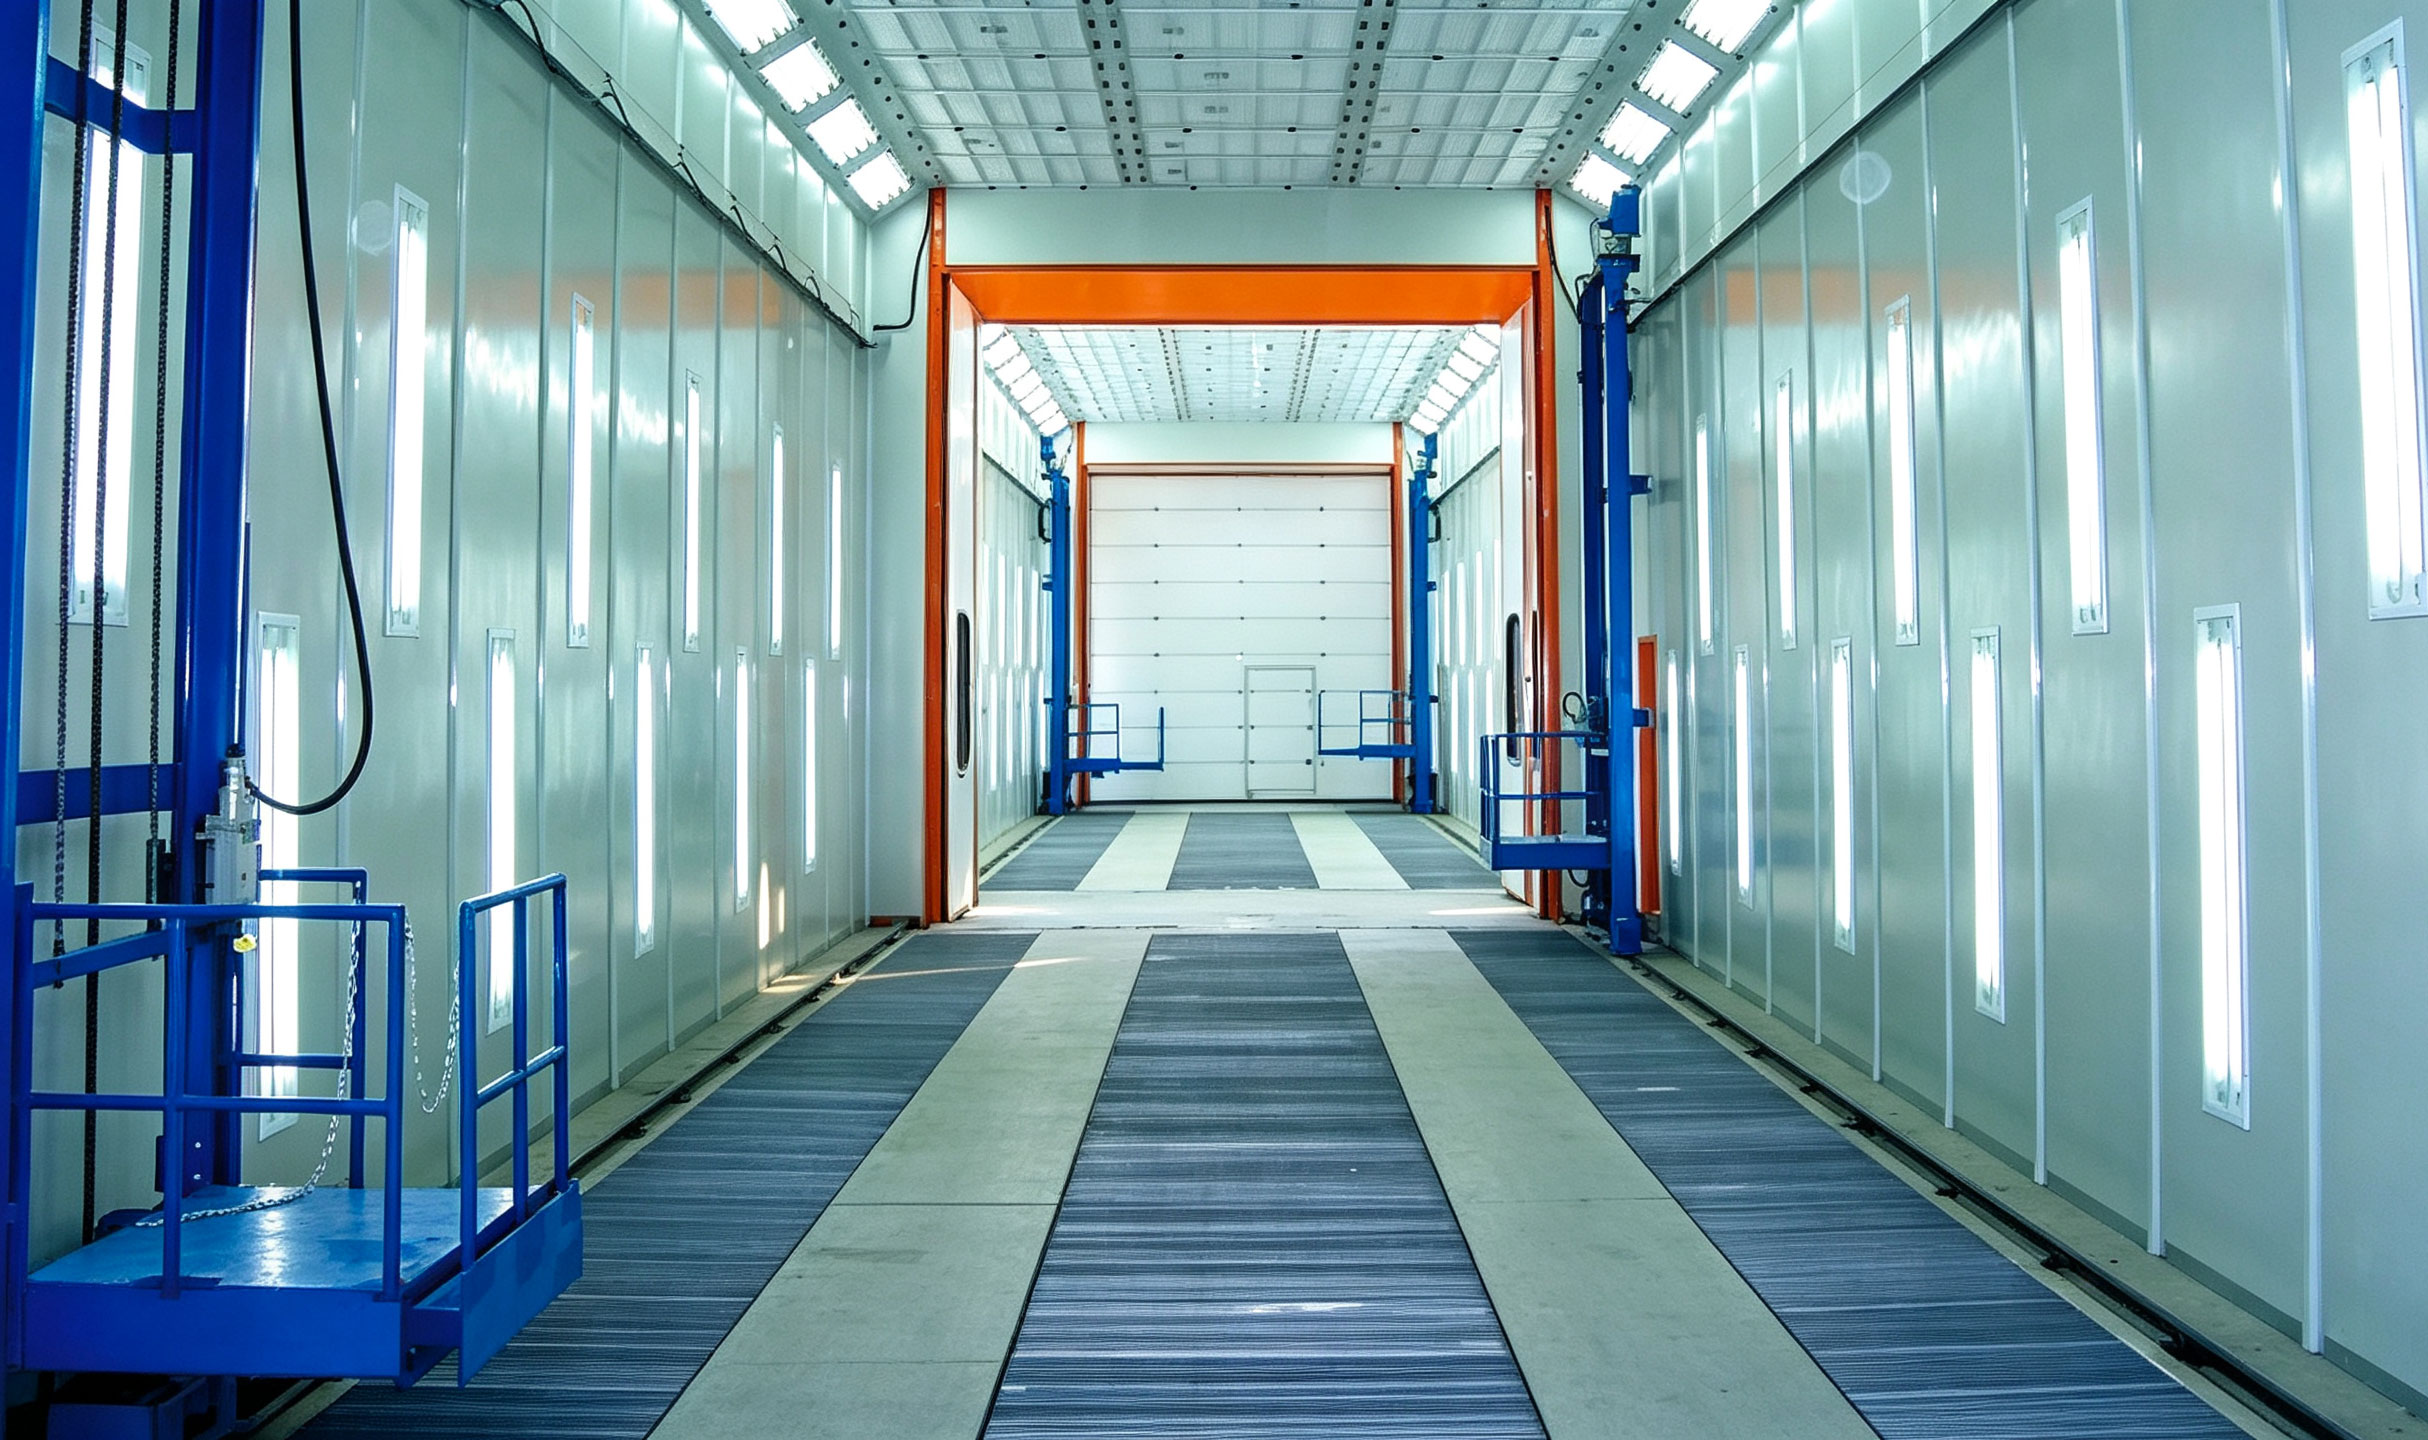
Pre treatment oil and dust removal → Spray room micro negative pressure and section wind speed stability → Closed loop of paint supply pressure/viscosity → Robot gun distance overlap constant (spray amplitude overlap about 50% -75%) → Leveling → Curing furnace temperature curve → VOCs treatment → PLC master control linkage. Ventilation cannot be started without spraying, and door locks cannot be short circuited. This is the bottom line of compliance.
打样阶段别只看“亮不亮”,按点测干膜厚度、色差ΔE、橘皮、附着力,留参数库。换产频繁的要离线编程+快速换色,把停机示教时间压下来。
During the sampling stage, don't just focus on whether it's bright or not. Measure the dry film thickness, color difference Δ E, orange peel, and adhesion by point, and keep a parameter library. Frequent production changes require offline programming and quick color changes to reduce downtime for teaching.
自动涂装线的账,算的是返工率、涂料利用率、换型时间,不是机器人多不多。
The account of the automatic painting line calculates the rework rate, paint utilization rate, and changeover time, not the number of robots.
 : 18563723072
 : sdcjtz@126.com
 : 山东省德州市齐河县经济开发区名嘉西路9号
扫码添加微信了解更多

 公司简介
 荣誉资质
 合作伙伴
 发展历程
 公司优势
 企业环境
 服务办事处
 创杰动态
 行业动态
 鲁公网安备 37142502000144号